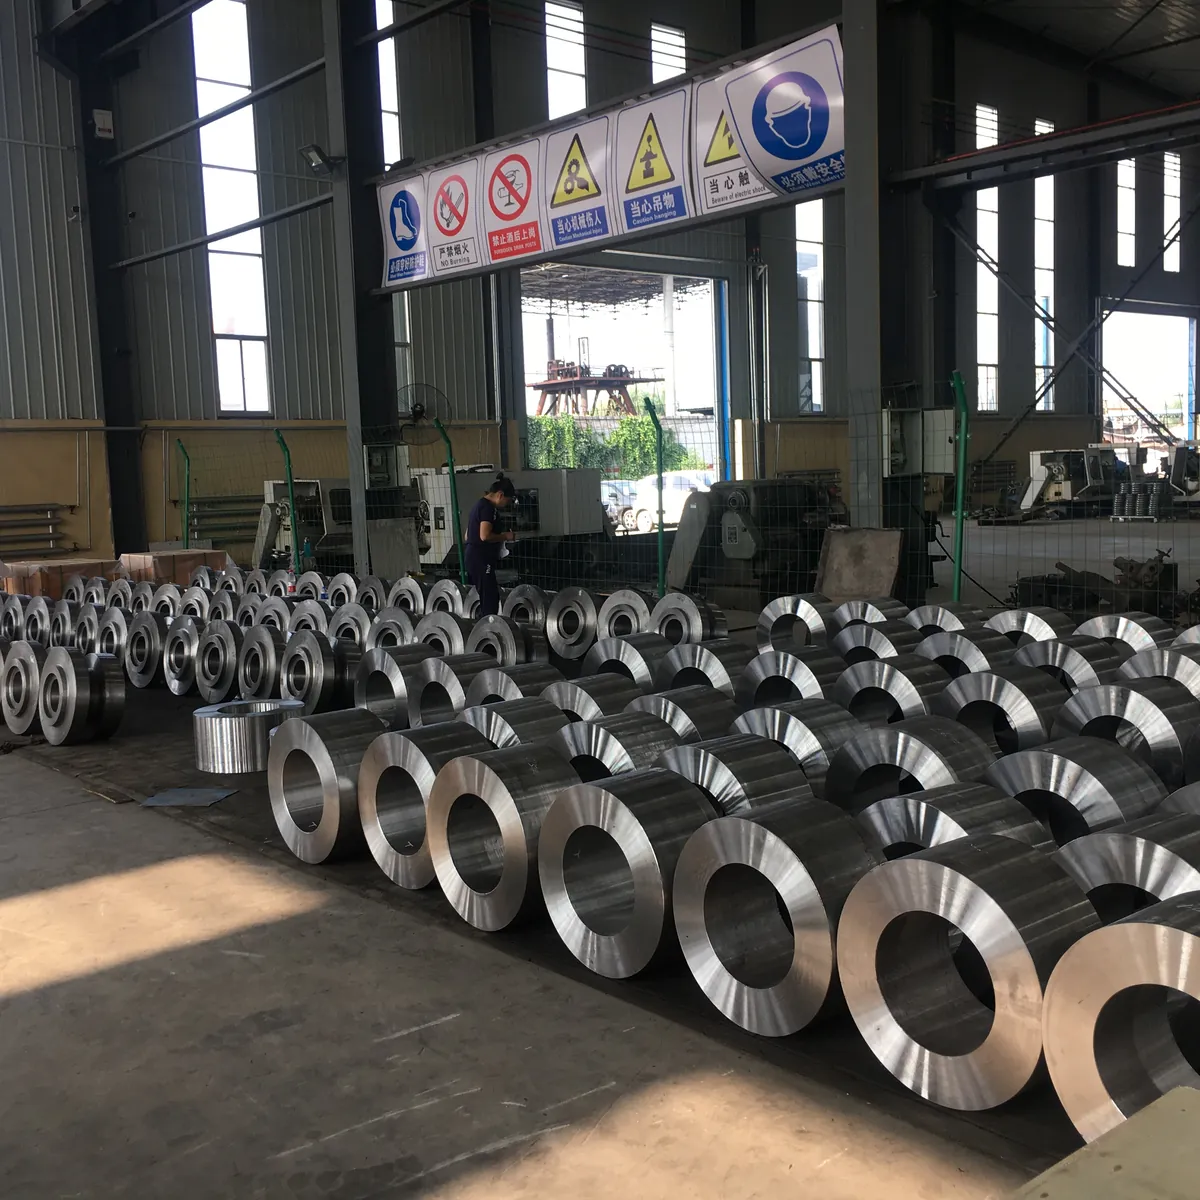
We roll rings up to 1,500 mm OD and 240 mm thick on our D51 ring rolling mill. Larger rings, up to 10,000 mm OD and 500 mm thick, are forged by partner forges near our plant in Dingxiang that run presses up to 10,000 t. Heavier-section or awkward proportions are open-die forged instead, and rings can be supplied as-forged, rough-machined or finish-machined. The drawing gives OD, ID, height, wall thickness, machining allowance and tolerance, and the material follows the ASTM or EN standard named on it.
These go into pressure vessels, bearing and gear blanks, rotating equipment, and wind, mining and power assemblies. Ovality and flatness after heat treatment are the real constraints on a large thin ring, so both should be stated rather than left to a general tolerance note. Inspection is UT, hardness, a dimensional report, the heat-treatment record, MTC 3.1 and traceability.